This study demonstrates the generation of hydrogen from aluminum cans via alkaline hydrolysis and the electrochemical recovery of aluminum and sodium compounds, enabling a recyclable, closed-loop reagent system.
A subscription to JoVE is required to view this content. Sign in or start your free trial.
Research Article
Hydrogen Production by Hydrolysis of Recycled Aluminum and Reagent Recovery by Electrolysis of the By-Product
In This Article
Summary
Abstract
Hydrogen is a promising energy carrier for achieving net-zero greenhouse gas emissions; however, its storage and distribution remain a challenge. This study shows a reproducible closed-loop protocol for on-demand hydrogen generation using aluminum beverage cans via alkaline hydrolysis, followed by electrochemical recovery of aluminum and sodium compounds from the reaction by-products. Aluminum cans are pretreated using combined thermal and chemical steps to remove polymer coatings and improve reactivity. Hydrogen is produced using sodium hydroxide solutions (3–5 M) and collected volumetrically, reaching a purity of 93.66% by volume, as determined by gas chromatography. The resulting sodium aluminate solution is processed in a two-compartment electrochemical cell, allowing precipitation of aluminum hydroxide (gypsite and bayerite phases) and the regeneration of sodium hydroxide at a concentration of 4.98 M ± 0.03 M. The energy consumption for the electrochemical recovery of aluminum hydroxide corresponds to an energy efficiency of 0.632 Wh・g⁻1. This work provides a practical framework for integrating hydrogen production with aluminum waste recovery in circular energy systems.
Introduction
The transition to net-zero greenhouse gas emissions requires the deployment of energy carriers that uncouple energy generation from consumption while enabling the large-scale integration of renewable resources. Currently, large-scale energy storage is dominated by pumped hydro, which accounts for more than 90% of global energy storage capacity. Other storage technologies, such as lithium-ion batteries, compressed air, and flywheels, remain limited in their scalability and cost-effectiveness for grid applications1,2,3.
In this way, hydrogen is widely considered a key vector for this transition due to its high gravimetric energy density and versatility in the energy, industrial, and chemical sectors4,5. It can be produced from a variety of sources, such as electrolysis of water with renewable electricity and hydrocarbon reforming.
However, widespread adoption of hydrogen technologies remains limited by challenges associated with storage, transportation, and infrastructure disposition. For example, traditional hydrogen storage methods, such as high-pressure compression (350–700 bar) or cryogenic liquefaction (-253 °C), require significant energy input, specialized infrastructures, and stringent safety measures, limiting their feasibility for large-scale deployment6,7,8.
Among the various hydrogen production strategies, metal-water reactions (aluminum hydrolysis) have become attractive options for on-demand hydrogen generation, especially in decentralized or off-grid applications9,10,11. Aluminum is particularly attractive in this context due to its abundance, high theoretical hydrogen yield (1.24 L·g⁻¹ Al), and compatibility with alkaline activation. The reaction between aluminum and water occurs through surface oxidation, forming aluminum hydroxide or aluminate species, while releasing hydrogen gas12,13,14. The hydrolysis of aluminum offers a high theoretical yield of hydrogen, as one mole of aluminum can generate 3 moles of hydrogen gas according to the reaction:
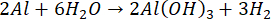 (1)
In practical systems, reaction kinetics and hydrogen yield are strongly influenced by surface passivation, alkaline concentration, and temperature. Typical sodium hydroxide concentrations suggested for effective aluminum hydrolysis range from 1–6 M. With higher concentrations, the removal of the aluminum oxide layer is accelerated, but corrosivity and safety requirements increase15,16,17. The reaction temperature affects both the rate of hydrogen evolution and the efficiency of aluminum consumption, with moderate heating (20–60 °C) usually sufficient to maintain rapid hydrogen generation18,19. These features highlight the importance of controlling pre-treatment and reaction conditions when evaluating the suitability of aluminum-based hydrogen generation for specific applications.
The hydrolysis reaction in water in the presence of sodium hydroxide may be described as
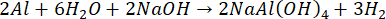 (2)
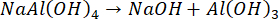 (3)
From a sustainability perspective, combining aluminum hydrolysis with the recovery and reuse of reaction by-products is fundamental to reducing material losses and the overall cost of the process. The sodium aluminate (NaAl(OH)4) formed during hydrolysis can be converted back into aluminum hydroxide and regenerated alkaline solutions through electrochemical or chemical processes, enabling closed-loop operation20,21. Recent studies have suggested that integrating waste aluminum feedstocks, such as post-consumer beverage cans, can significantly improve the economic and environmental performance of hydrogen production systems by reducing feedstock demand and diverting waste from landfills22,23.
Although several aluminum-water systems have been proposed at the laboratory scale, challenges remain related to scalability, process integration, and energy efficiency. Specifically, few protocols provide sufficient procedural details to enable reproducible implementation across the pre-treatment, hydrogen generation, gas handling, and reagent recovery stages24,25.
Therefore, this study reports this gap by describing a fully integrated laboratory-scale system for hydrogen production from recycled aluminum via alkaline hydrolysis, followed by electrochemical recovery of aluminum and sodium compounds. By combining practical operating ranges with detailed procedural guidance, this method aims to support reproducibility and facilitate the evaluation of hydrogen generation from aluminum in circular energy systems.
Access restricted. Please log in or start a trial to view this content.
Protocol
1. Pre-treatment of aluminum sheets
- Initial preparation of aluminum cans
Aluminum beverage cans (473 mL) were collected and thoroughly rinsed with tap water and dishwashing detergent to remove residual liquids and sugars. The cans were subsequently rinsed with deionized water and allowed to air dry at room temperature. The top and bottom ends of each can were removed using metal scissors, retaining only the cylindrical body. The aluminum body was then cut and flattened into sheets, which were further divided into pieces of the desired size (4 mm2 or 1 cm2). - Thermal pre-treatment with acetone
The aluminum pieces were placed in a laboratory autoclave and heated to 121 °C for 30–45 min to facilitate softening of the polymer coatings. After completion of the heating cycle, the autoclave was allowed to cool naturally to room temperature before being opened. The aluminum samples were transferred to 50 mL polypropylene tubes, and sufficient acetone was added to fully submerge the pieces. The tubes were sonicated in an ultrasonic bath for 15–20 min at room temperature. During sonication, the acetone solution gradually acquired visible coloration due to dissolution of the paint layer, at which point sonication was discontinued. The acetone was filtered using a glass funnel and collected in a labeled waste container. The acetone treatment and sonication process was repeated up to four times, or until no visible coloration of the solvent was observed. - Calcination pre-treatment
Following acetone treatment, the aluminum pieces were placed in ceramic crucibles, ensuring that the samples were not stacked. The crucibles were transferred to a muffle furnace and heated to either 200 °C or 500 °C for 2 h under ambient air conditions. After calcination, the furnace was switched off and allowed to cool naturally to below 100 °C with the door kept closed. The crucibles were then removed and immediately transferred to a desiccator to cool to room temperature, minimizing moisture absorption. - Visual inspection and acceptance criteria
The treated aluminum surfaces were visually examined under ambient lighting conditions. Proper pre-treatment was confirmed by the absence of visible paint residues and the presence of a uniformly metallic or slightly oxidized surface appearance. Samples exhibiting thick rust flakes or incomplete coating removal were excluded from further use.
2. Hydrogen generation by aluminum hydrolysis
- Assembly of the hydrogen generation system (Figure 1)
A closed hydrogen generation system was assembled using a three-necked round-bottom flask serving as the reactor, a water-filled check valve to prevent backflow, two condensers connected in series, and an inverted burette for gas collection. The gas outlet of the reactor was connected to the check valve, followed by a first condenser operating at room temperature and a second condenser supplied with cold water (~0 °C). The outlet of the second condenser was connected to an inverted burette filled with deionized water and equipped with separate shut-off valves for water and gas. All joints and connections were inspected for leaks by applying slight pressure with an inert gas or by confirming the absence of bubble formation when submerged connections were briefly pressurized. - Preparation of the alkaline solution
A sodium hydroxide solution at the desired concentration (typically 5.0 M) was prepared using deionized water. The solution was allowed to cool to room temperature prior to use to prevent uncontrolled temperature increases during the hydrolysis reaction. - Initiation of aluminum hydrolysis
Approximately 0.40 g of pretreated aluminum pieces was introduced into the reactor flask. A temperature probe was inserted through one of the flask necks, ensuring that the probe tip remained submerged in the liquid phase during the reaction. All necks of the reactor were sealed except for the reagent inlet and gas outlet. Subsequently, 15.0 mL of the prepared 5.0 M sodium hydroxide solution was added through the reagent inlet, and the reactor was immediately sealed to initiate the hydrolysis reaction. - Monitoring hydrogen evolution
Reactor temperature and internal pressure were recorded at 1-s intervals for 60 min using a data acquisition system. Hydrogen evolution was observed as a continuous gas flow passing through the condensers and into the inverted burette, which functioned as a water-sealed graduated cylinder for volumetric measurement by water displacement while preventing air ingress. The reaction was maintained without external heating unless the temperature decreased below 20 °C, in which case, gentle external heating was applied to sustain gas evolution. - Measurement of hydrogen volume
At the conclusion of the reaction, the system was allowed to equilibrate to room temperature. The water levels inside and outside the inverted burette were adjusted to the same height prior to recording the final gas volume. The collected gas volume, room temperature, and atmospheric pressure were documented. The amount of hydrogen produced was subsequently calculated using the ideal gas law. - Gas sampling for purity analysis
For gas purity assessment, the inverted burette was replaced with a gas sampling bag. Gas was collected after stable hydrogen evolution had been established. The sampling bag was sealed immediately following collection, and the gas composition was analyzed using gas chromatography.
3. Electrochemical recovery of aluminum and sodium compounds
- Assembly of the electrochemical recovery cell (Figure 2)
The ion-exchange membrane was activated by immersion in 0.5 M aqueous sodium hydroxide solution for at least 24 h at room temperature. After activation, the membrane was thoroughly rinsed with distilled water to remove excess electrolyte. An electrochemical cell consisting of two compartments separated by an ion-exchange membrane was assembled (Figure 2), ensuring proper sealing to prevent liquid crossover between compartments26. A graphite electrode was installed as the anode in one compartment, while a stainless-steel electrode served as the cathode in the opposite compartment. The electrodes were connected to a direct current power supply, and the correct polarity was verified prior to operation. - Preparation and loading of electrolytes
The liquid residue obtained after aluminum hydrolysis, consisting of a sodium aluminate solution, was transferred to the anode compartment of the electrochemical cell. A 3.0 M sodium hydroxide solution was added to the cathode compartment to function as the supporting electrolyte. The initial volumes introduced into each compartment were recorded. The final electrolyte composition consisted of approximately 200 mL of sodium aluminate solution in the anode compartment per batch and 3.0 M sodium hydroxide solution in the cathode compartment. - Electrochemical operation
Electrolysis was initiated by applying a constant voltage of 4.5 V to the cell. The process was maintained under constant voltage conditions while the current, typically around 5.5 mA, was continuously monitored. Voltage, current, and elapsed time were recorded at regular intervals, such as every 10 min. Electrolysis was continued until the pH measured in the cathode compartment remained stable for at least 30 min. - Recovery and post-treatment of aluminum hydroxide
During electrolysis, the anode compartment was periodically observed for the formation of a white precipitate. The generation of aluminum hydroxide was indicated by the appearance of a fine, white, gelatinous solid suspended in the solution. Electrolysis was terminated once precipitate formation ceased and the cathode pH stabilized. The precipitated aluminum hydroxide was collected by vacuum filtration using fine-pore filter paper and washed repeatedly with deionized water until the filtrate reached neutral pH. The recovered solid was dried in an oven at 60 °C for 12 h and subsequently allowed to cool to room temperature in a desiccator before its mass was recorded. The crystalline phase of the recovered material was identified using X-ray diffraction analysis, confirming characteristic peaks corresponding to aluminum hydroxide phases. - Recovery of regenerated sodium hydroxide
Following electrolysis, the cathode solution was collected and stored in an airtight container. The concentration of regenerated sodium hydroxide was determined by acid–base titration prior to reuse. - Calculation of energy efficiency
The total electrolysis time and average current were recorded during operation. The electrical energy consumed (EC) was calculated using the equation:
EC (Wh) = Voltage (V) × Current (A) × Time (h)
The energy efficiency (EE) of aluminum hydroxide recovery was determined by dividing the total energy consumed by the mass of aluminum hydroxide recovered, expressed in Wh·g⁻1.
Access restricted. Please log in or start a trial to view this content.
Results
The success of the pre-treatment of recycled aluminum cans is confirmed by visual inspection and X-ray diffraction (XRD) analysis (Figure 3). After combined treatment with acetone and calcination, the aluminum surfaces exhibited a uniform metallic appearance. Although the dominant diffraction peaks correspond to metallic aluminum (JCPDS 04-0787), additional minor features are assigned to residual surface oxides, particularly in samples subjected to incomplete pre-treatment or in regions wher...
Access restricted. Please log in or start a trial to view this content.
Discussion
Previous studies have described various pre-treatment and activation strategies to improve aluminum hydrolysis in water, including mechanical and mechanochemical activation (e.g., ball milling or magnetic activation), galvanic activation with metal additives, liquid metal activation, chemical etching, and heat treatments30,31,32,33,34. Although mechanochemical...
Access restricted. Please log in or start a trial to view this content.
Disclosures
The authors have nothing to disclose.
Acknowledgements
The authors acknowledge the technical help received from Ms. Maria Luisa Ramón for the XRD analysis. The funding for the work came through the project DGAPA-UNAM IN108325.
Access restricted. Please log in or start a trial to view this content.
Materials
| Name | Company | Catalog Number | Comments |
|---|---|---|---|
| Acetone, ACS reagent (≥99.5%) | Jalmek | A0425 | Removal of paint and polymeric coatings |
| Aluminum beverage cans (473 mL) | Local collection | N/A | Post-consumer aluminum feedstock |
| Analytical balance | Boeco | BAS 31 Plus | Mass measurements |
| Benchtop autoclave | Ecoshel | CVQ-280d | Thermal pretreatment |
| Data acquisition software | In-house programmed | N/A | Temperature and pressure logging |
| DC power supply | Matrix | MPS-3002L-3 | Electrolysis operation |
| Deionized water (18.2 MΩ·cm @ 25°C) | Millipore Milli-Q (in-house) | N/A | Preparation of solutions and washing steps |
| Desiccator | Glass laboratory type | N/A | Cooling and moisture control |
| Drying oven | Binder | RF115-UL | Drying aluminum hydroxide |
| Gas chromatograph | Agilent Technologies | 7890B | Hydrogen purity analysis |
| Graham condenser (300 mm) | N/A | N/A | Primary condenser |
| Graphite electrode (anode) | Fuel Cell Earth | Isomolded Graphite Plate | Electrochemical oxidation |
| Ice / ice bath | Local supply | N/A | Cooling condenser to ~0°C |
| Inverted burette (1000 mL) | Custom-built | N/A | Volumetric hydrogen measurement |
| Muffle furnace | Yamato | FO100CR | Calcination of aluminum samples |
| Nafion 212 membrane | DuPont | NRE 212 | Proton exchange membrane |
| pH buffer solutions (CRM) | Fermont | S1015, S1025, S1035 | Calibration of pH meter |
| pH meter | Thermo Scientific | Orion Star A211 | Monitoring catholyte pH |
| Phenolphthalein indicator | Sigma-Aldrich | 319236 | Endpoint detection in titration |
| Potassium hydrogen phthalate (CRM) | MilliporeSigma Supelco | 11-101-5732 | Acid–base titration standardization |
| Pressure sensor | Bosch | BMP180 | Monitoring reactor pressure |
| Secondary condenser | Custom-built | N/A | Moisture removal from hydrogen gas |
| Sodium hydroxide (NaOH) pellets | Fermont | 36902 | Preparation of alkaline solutions (3–5 M) |
| Stainless steel electrode (cathode) | Fuel Cell Earth | 304 SS 120 Mesh | Electrochemical reduction |
| Temperature sensor & data logger | Custom-built | N/A | Monitoring hydrolysis reaction |
| Three-neck round-bottom flask (150 mL) | DesChem | N/A | Hydrogen generation reactor |
| Two-compartment electrochemical cell | Custom-built | 500 mL per cell | Electrochemical recovery |
| Ultrasonic bath | Branson | 1510 | Acetone-assisted paint removal |
| X-ray diffractometer (XRD) | Rigaku | Ultima IV | Phase identification |
| XRD analysis software | Manufacturer-provided | N/A | Phase identification |
Reprints and Permissions
This article has been published
Video Coming Soon